Best Practices for Industrial Surplus Management

Why Idle Automation Stock Becomes a Sourcing Problem
A discontinued drive sits on a shelf for four years, gets scrapped, and eighteen months later the same part number triggers a 20-week OEM lead time and a stopped line. That is the loop industrial surplus management exists to break. At Automa.Net, buyers can search for legacy Siemens or Allen-Bradley components, while sellers can list surplus stock.
Surplus is not a storage problem. It is a sourcing problem deferred. Every pallet of idle assets may represent recoverable working capital or a future sourcing need.
Below, we lay out the disposition framework, the identification steps, and the governance that keeps surplus from rebuilding. The approach is built for MRO teams and distributors who already know their BOM, not for people learning what a PLC is.
Best Practices for Industrial Surplus Management: The Disposition Framework
Industrial surplus management is the structured process of identifying, valuing, tracking, and disposing of excess, obsolete, and idle automation stock so it either returns capital or returns to service. The core discipline is deciding fast, per item, instead of letting stock sit until it has no value at all.
The framework below sets out possible routes for each line item, not just retain or sell.
- Identify the part: nameplate, part number, revision, condition, and the machine it came from.
- Classify demand: still used on an active machine, used on a legacy machine, or used nowhere in your installed base.
- Value it against current market availability and condition, not original purchase price.
- Route it to one of seven disposition channels (below).
- Record the decision, the approver, and the date so the same item does not re-enter the pile next year.
The Seven Disposition Routes
Retain and sell are not the only options. Match the route to condition, demand, value, and urgency.
| Route | When it fits | What it recovers | Watch out |
| Reuse in-house | Part serves an active or legacy machine you still run | Avoided OEM spend and downtime | Requires a verified spare-parts list per machine |
| Redeploy | Part fits another site or line in your group | Internal transfer value | Inter-site logistics and ownership transfer |
| Resale as surplus | Demand exists in the independent market | Highest net recovery when demand is live | Condition documentation and buyer verification |
| Return to vendor | Part is current, under warranty, or part of a recall or exchange program | Credit or replacement | OEM return windows are usually short |
| Refurbish then sell | Repairable drive, motor, or HMI with test documentation | Higher price than as-is | Repair cost must be netted against recovery |
| Recycle | No demand, no reuse path, but material value exists | Scrap or material value | Data and control-system removal first |
| Dispose | Hazardous, damaged, or fully obsolete with no market | Compliance, not value | Regulatory and environmental obligations |
The decision order depends on the part's condition, demand, value, and urgency. Consider reuse, redeployment, resale, return-to-vendor, refurbishment, recycling, or disposal as applicable.
Valuing a Part Before You Route It
Consider market availability and condition alongside the original purchase price. Ask whether there is demand, whether the part can be verified, and how long it may take to sell.
OEM vs Refurbished vs Surplus: Which Channel Fits
Channel choice decides both cost and risk, so match the channel to the machine's criticality rather than to habit.
| Channel | Lead time | Cost position | Best for | Watch out |
| OEM new | Longest, often extended for legacy parts | Highest | Warranty-critical, safety-relevant assets | Discontinued lines may never return |
| Refurbished | Short to medium | Mid | Repairable drives, motors, HMIs | Verify test documentation |
| Surplus | Shortest when in stock | Lowest | Obsolete parts, spares for legacy machines | Condition varies by lot |
Surplus may be one channel to consider for legacy equipment. Verify what you are buying. For a deeper comparison of channel trade-offs, read our guide on OEM vs aftermarket industrial parts.
Obsolete Industrial Parts Management Starts With Identification
Correct identification is important when sourcing or selling obsolete industrial parts. A revision mismatch can complicate sourcing, so confirm the exact variant.
Compare the physical item with its records. A nameplate can help confirm the part details.
Reading a Nameplate Before You Search
Photograph the nameplate before anything else. Capture the full type designation, the order number, the serial number, and the revision or firmware level. On Siemens drives, the order number with its suffix matters; on Allen-Bradley, the series letter changes compatibility.
Two habits cut mis-identification sharply. First, record the nameplate image alongside the part in your stock list, not just the typed number. Second, note the machine the part came from; that context tells a buyer whether the part is a working pull or an unknown.
You can use AutomaSnap to identify parts from a nameplate photo.
Surplus Parts Tracking Without an ERP Project
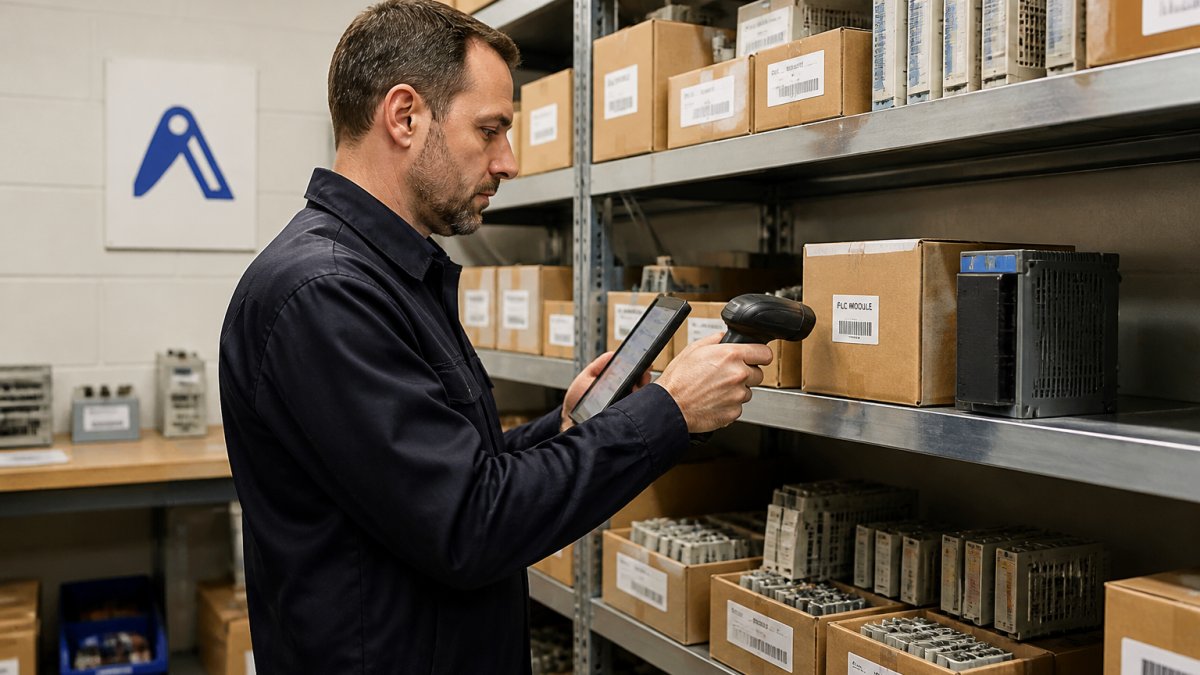
A structured spreadsheet with defined fields and periodic physical counts is one way to track surplus parts.
The minimum viable record per item: part number, nameplate photo, condition, quantity, location, date received, and a disposition status.
You can review items that have not moved against the current machine population.
For teams that want the full implementation detail, our guide on implementing industrial spare parts tracking covers the field structure and review cadence.
How to Sell Surplus Industrial Equipment Without Giving It Away
When selling surplus industrial equipment, consider the intended buyer and the available sales channels.
Before listing, prepare records, nameplate photos, and condition notes. You can group items by machine family for buyers sourcing a legacy line.
Find it on Automa.Net →
Then choose a channel for reaching potential buyers. Sellers can list surplus stock through Surplus Solutions.
Consider whether the installed base and demand for a part may affect its resale prospects.
Obsolete Automation Parts Sourcing When the OEM Lead Time Is 20 Weeks
Sourcing obsolete automation parts can be time-sensitive when downtime is a concern.
One approach is to confirm the exact part number and revision from the nameplate, then search the independent market.
You can broadcast a requirement through a request board. Our guide on sourcing obsolete industrial components covers verification and fallback options when nothing is in stock.
Watch out: a part that matches on number but not on revision or firmware can fail on commissioning.
KPIs and Governance That Keep Surplus From Rebuilding
Surplus rebuilds when nobody owns the decision. Governance is the difference between a one-time cleanout and a process that holds. Assign one owner for surplus disposition and one review cadence, monthly for fast-moving MRO stock and quarterly for slow-moving legacy spares.
Who Owns What
Surplus crosses functions, so name a role for each step rather than leaving it to the storeroom.
- Maintenance identifies the part, confirms condition, and states whether it is still needed on an active machine.
- Procurement values it against market availability and chooses the disposition route.
- Finance approves write-offs and records recovery value.
One person coordinates the loop; the decisions stay with the function that holds the knowledge. Without that split, either nobody decides or one team decides everything and the others ignore it.
The Measures That Matter
Track a small set of measures rather than a dashboard nobody reads. Define each one so the number means the same thing every month.
| Measure | How to calculate | What it tells you |
| Inventory turnover on spare parts | Cost of parts consumed in the period divided by average spare-parts stock value | Whether stock is moving or accumulating |
| Days on hand | Average stock value divided by average daily consumption | How long current stock would last at present use |
| Value of stock untouched beyond the review period | Sum of stock value with no movement since the last review | The size of the surplus problem |
| Parts flagged obsolete but still held | Count of items with no installed base and no disposition decision | Decision backlog |
| Recovery value realised from disposals | Sum recovered from resale, return-to-vendor, and recycling | Whether the program pays for itself |
| Downtime events caused by a missing part | Count of stoppages traced to a part you had written off or scrapped | Whether retention decisions were right |
Recovery value and downtime events can help assess the results of a surplus program and retention decisions. Scrapping a part that is later needed can create additional costs.
The Approval Workflow
You can set a decision deadline as well as a review date. Record the approver and date against each item to document the decision.
Review the disposition status of flagged items on a fixed schedule, and reconcile the physical count against the record. Parts pulled for repairs can be missed in records, so a physical count can help identify discrepancies.
For a fuller set of supply chain measures, see our supply chain KPI guide.
Start With a Single BOM or Nameplate on Automa.Net
You can start with one part. Pick a single BOM line or nameplate from your idle stock and review its identification, classification, and routing.
You can search for a part across the network with AutomaSEARCH, or broadcast an RFQ through the Request Board.
Frequently Asked Questions
How do you decide whether to reuse, sell, or scrap surplus parts?
Work through four checks in order. First, does the part still serve a machine you run or a machine you support? If yes, keep it as critical spares and log it. Second, is it still available from the OEM, or discontinued? Discontinued stock has resale value to buyers running legacy lines. Third, can you verify condition and completeness? Condition and documentation can be relevant when deciding whether to reuse, sell, or scrap a part. Fourth, consider whether disposal carries regulatory obligations. Use these checks to inform your choice of reuse, resale, or scrap.
How do you track surplus and obsolete automation components?
Surplus parts tracking fails when it depends on memory. Give every item a permanent location and record the manufacturer part number exactly as printed on the nameplate, plus the quantity and the date it entered storage. A spreadsheet with those four fields is one possible tracking method. Review the list on a fixed cycle and flag anything that has not moved. For items you cannot identify, photograph the nameplate and use a part identification tool rather than guessing the number.
How can you verify surplus industrial parts before buying them?
Ask for the exact manufacturer part number and compare it against your BOM, not against a product photo. Request the nameplate image, confirm the firmware or hardware revision where it matters, and check whether accessories, terminal covers or memory modules are included. Buy from sellers who list real stock rather than catalogue entries. On Automa.Net, AutomaSEARCH lets you search across the network, and the Request Board lets you broadcast RFQs.
How can manufacturers sell surplus automation stock?
When selling surplus industrial equipment, you can group stock by manufacturer and part number, state condition, and photograph nameplates. Consider your sales channel before listing. Automa.Net's Surplus Solutions lets sellers monetise surplus and overstock.
What is the 80/20 rule for inventory in a spare parts store?
You can rank stock by issue frequency and the operational importance of a failure. Reviewing items that have not moved can help identify stock for further assessment.
How do you avoid excess inventory building up again after a cleanout?
Fix the intake, not just the shelf. Require a part number and a storage location before anything is booked in, and set a rule that stock without a linked machine or work order gets reviewed after a defined period. Give one person ownership of the surplus list and a fixed review date. When a machine is decommissioned, treat its spares as a disposition task on the shutdown checklist rather than something to sort out later. Those controls can help you review stock intake and surplus decisions.
The challenge is not knowing the framework; it is applying it to stock that has sat untouched for years. Automa.Net connects you to a verified network of suppliers with real, in-stock inventory, so a discontinued part number becomes a search rather than a shutdown. Get started with Automa.Net and turn your first idle part into either recovered capital or a working spare.
Find it on Automa.Net →
Other Posts

Alternatives to Discontinued Allen-Bradley Servo Motors
Find discontinued Allen-Bradley servo motor alternatives. Compare OEM replacements, cross-brand swaps and refurbished units.
Read More →
Why Legacy Industrial Equipment Needs Better Stock Visibility
Poor stock visibility on legacy machines hides which spare parts exist and fit. Learn how retrofit gateways link consumption to your stock ledger.
Read More →
Sourcing Legacy Automation Components in Europe: 2026 Guide
Sourcing legacy automation components in Europe means identifying parts, vetting suppliers and managing cross-border risk.
Read More →